
 English
 French
 Deutsch
 العربية
 Español
 Русский
 にほんご
 Português
 한국어
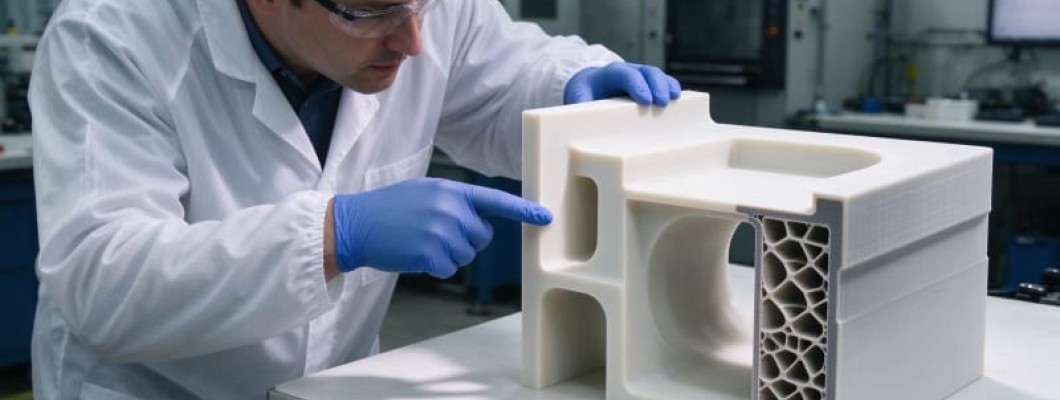
What rapid prototyping really means
rapid prototyping is not printing a shape and calling it a product. It is the controlled step between a CAD file and a testable part, where a qualified 3d printing prototype service builds, finishes and inspects a part against the exact questions the design team needs answered. A prototype exists to validate fit, form, function or market reaction before tooling money is spent. For B2B product teams that means compressing months of design iteration into days, without committing to injection mould tools or CNC fixtures that lock in geometry too early.
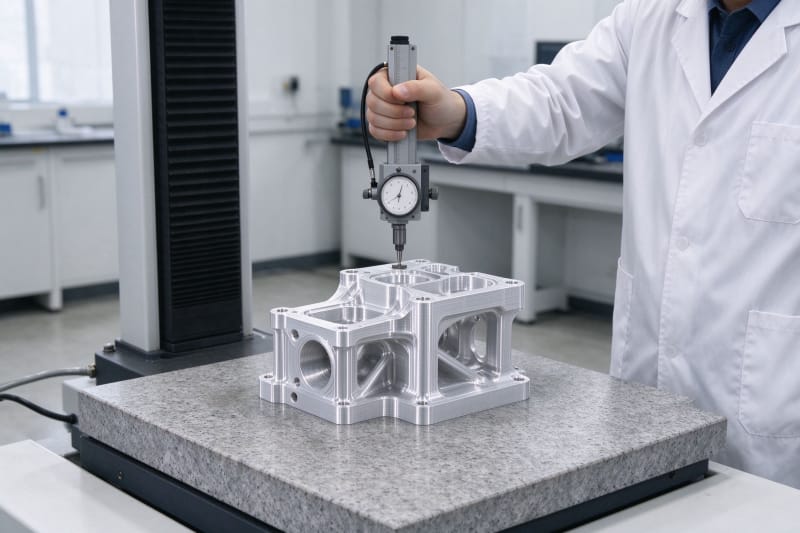
The difference between a hobby print and a serious prototype is the process around the printer. A hobby print ships as it comes off the bed. A custom 3d printing service reviews the geometry, selects the process and material for the real test case, runs first article checks, and records the route so the next iteration builds on the last. That is why teams that treat rapid prototyping 3d printing as a throwaway exercise usually get a throwaway part, while teams that specify tolerances, load case and test conditions get a prototype that teaches them something useful.
What to specify before requesting a prototype
The most common reason a prototype disappoints is not the printer, it is an underspecified request. A file alone tells the supplier the shape, but not what the prototype must prove, which dimension must hold, how it will be loaded, or whether it needs a cosmetic surface or a functional one. Serious suppliers ask for these details before quoting, because each answer changes process, material, orientation and price. The table below lists the fields a B2B buyer should fill in before sending any file, and why each one matters.
|
Choosing the right process for your prototype
There is no best prototyping process, only the right one for the question being asked. FDM is fast and cheap for large concept models and low stress housings, but layer lines and anisotropy make it a poor choice for sealing faces or loaded brackets. sla printing service and resin processes give smooth surfaces and fine detail, ideal for master patterns, cosmetic parts and small ducting, but engineering resins must be matched to temperature and UV exposure. SLS and MJF in nylon produce functional prototypes with good isotropic strength, no supports and easy nesting. Metal powder bed fusion is for prototypes that must carry load, survive heat or replace machined alloy components, and it carries a different cost and lead time.
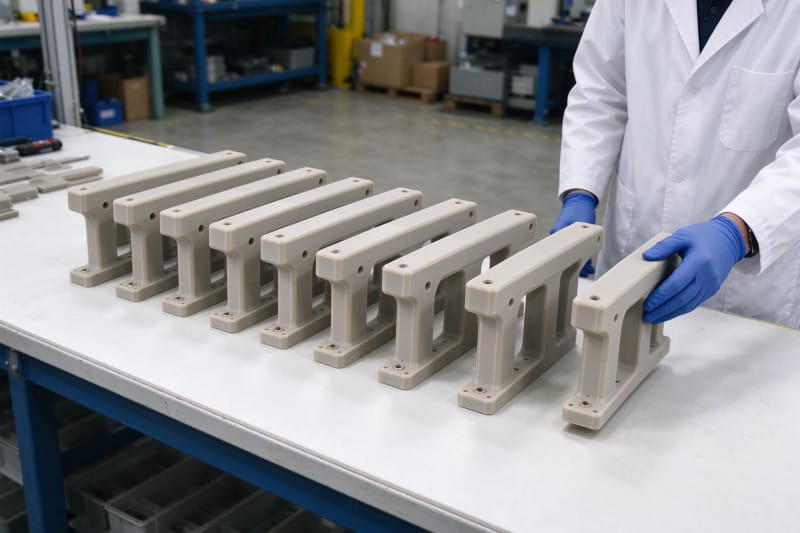
Material follows the test, not preference. A buyer who asks for the strongest material usually gets a part that is too brittle, too expensive or too hard to finish. A bracket that sees shock may need a tough nylon or carbon filled polymer rather than the stiffest resin. A part that lives in sunlight needs UV stable material or a coating. A part that must be food contact or medical grade needs a qualified material and a controlled process, not just a polymer name. A good supplier recommends by function, and explains the trade off rather than upselling the most expensive powder.
Design for prototyping speed and cost
Prototyping is not free geometry. Every process has limits, and ignoring them shows up as support marks, warped walls, trapped resin or a price that surprises the buyer. The first DFM rule is wall thickness: too thin and the part warps or fails, too thick and it wastes material and build time. The second is orientation: the face that must be smooth should not sit on supports, and the face that must be flat should be printed flat or machined after. The third is drainage and access: resin parts need drain holes, powder parts need depowder access, and internal channels must be reachable for cleaning and inspection.
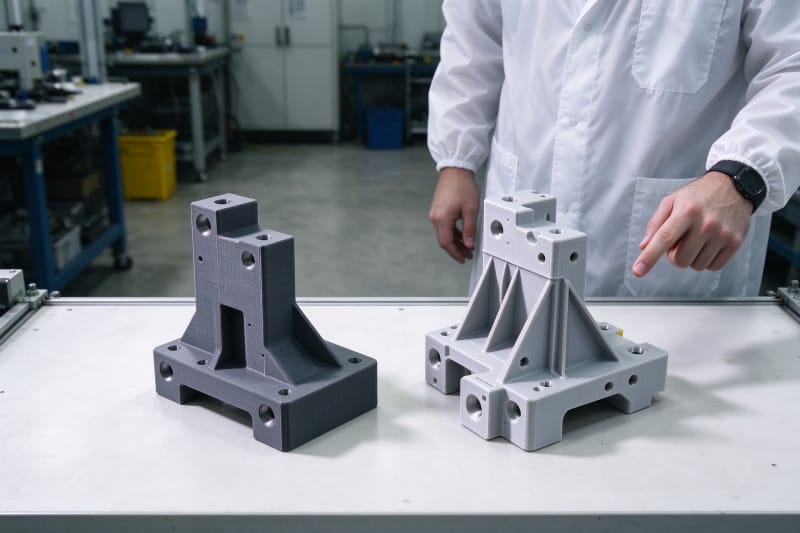
Cost in prototyping is mostly build volume and machine time, not material weight. A part that is 20 percent larger can cost 50 percent more because it occupies more of the build area and forces fewer parts per run. Hollowing, lattice filling and nesting reduce cost without changing function, but they must be designed in, not requested after the quote. Buyers who share the assembly context get better DFM advice, because the supplier can see which walls are cosmetic, which are loaded, and which can be lightened.
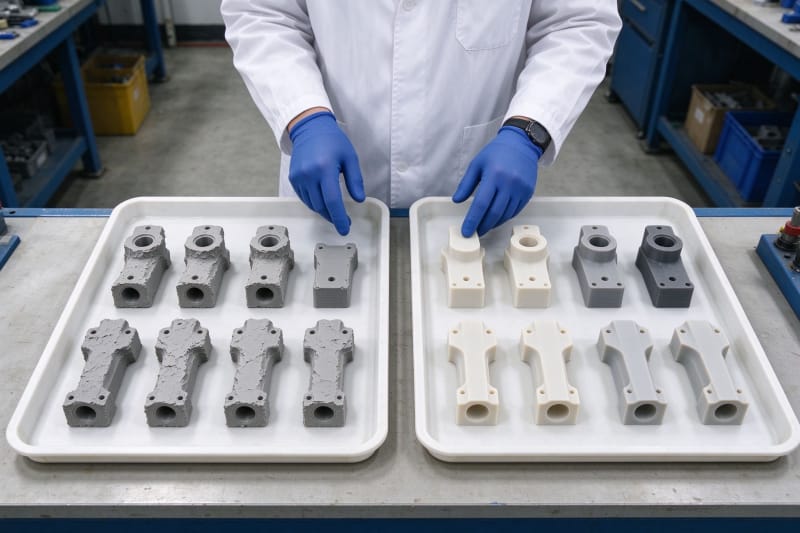
Most prototyping problems are predictable before the first layer. A wall that is too thin, a hole that is below resolution, or a cavity that cannot be drained will fail the same way on every machine, so a serious supplier flags them at the quote stage rather than discovering them on the bed. The buyer who receives a DFM note with the quote, instead of a surprise after shipment, is working with a supplier that treats prototyping as a controlled engineering step. The table below lists the most common DFM issues buyers send, and how they are fixed before production.
Common DFM issue | What goes wrong in production | Typical fix |
Wall below process minimum | Warping, break out, failed print | Thicken to qualified range or add ribs |
Large flat unsupported face | Curling, layer separation, poor flatness | Orient flat, add brim, or machine face |
Sealed internal cavity | Trapped powder or resin, weight gain | Add drain holes, hollow or lattice fill |
Tight hole below process resolution | Oversize or closed hole, no fit | Print undersize and ream, or tap after |
Critical face on support side | Support marks, rough surface, rework | Reorient part or plan CNC finishing |
Quality gates for prototype production
A prototype is only as good as the checks between print and ship. A serious shop runs incoming material checks, first article dimensional checks, and process records per build. For functional parts it may run density tests, coupon tests or CMM inspection on critical dimensions. For cosmetic parts it checks surface finish, colour and support removal. The buyer should know which checks are standard and which are chargeable, because a quote that omits inspection looks cheaper until the first bad batch arrives.
This is where HUANYA keeps the three things B2B buyers hate most out of the box. First, dimensional stability across iterations: the second revision matches the first in critical dimensions because the process, material lot and inspection route are locked, not reinvented each run. Second, on time delivery: builds are scheduled against real machine availability, so the promised date is a plan, not a hope. Third, consistent post processing: bead blast, support removal and finishing follow one written route, so surface quality does not drift between iterations. Cheap shops sell the printer, HUANYA sells the qualified route around it.
From prototype to low volume production
A prototype proves the design, but the real value comes when the design is ready to move into low volume production. The transition is not automatic: a part that prints well as a one off may need redesign for nesting, for consistent material properties, or for post processing that scales. Buyers who plan for production from the first prototype get better advice, because the supplier can flag geometry that will become expensive at fifty units rather than at five. The goal is not to print the same part forever, it is to use each prototype to remove risk before the next commitment.
Reorders are where prototyping proves its value. The first order proves the design, the second order proves the supplier. A buyer who returns two weeks later with a revised file should receive a part that builds on the first, with the same quality baseline and a clear record of what changed. HUANYA reviews each revision for better nesting without changing the approved geometry, and tells the buyer when a small design change would lower cost without touching function. The material lot is logged, the process is recorded, and the buyer is never surprised by a part that looks the same but does not fit.
Pricing transparency and hidden costs
A prototype quote should be readable, not mysterious. The unit price is built from material, machine time, post processing, inspection and overhead, and a transparent supplier lists what is included and what is extra. The most common hidden costs are expedited handling, special packaging, material certificates, CMM reports, and rework after first article. A quote that looks cheap often omits one of these, and the buyer pays later. A quote that lists everything looks higher at first, but it is the real cost of a part that fits and lasts.
Buyers should compare quotes on the same route, not on the same number. Two suppliers quoting the same file can produce very different prices because one includes bead blasting and the other ships as printed, one runs CMM and the other checks by eye, one uses certified material and the other uses open stock. The right comparison is alloy or polymer, process, post processing, inspection and lead time, side by side. Once the routes match, the price comparison is fair, and the cheapest qualified route usually wins.
Prototype with HUANYA
Upload your STEP or IGES file to HUANYA, name the prototype purpose, the critical dimensions, the load case and the finish, and receive a quote that lists process, material, post processing and inspection instead of one bare number. Compare it on the same route, and the right rapid prototyping partner usually becomes clear on the first read.


Leave a Comment